Optical Liquid Level Sensors: A Complete Overview and Technology Guide
This article is the encyclopedia entry for the optical liquid level sensor cluster - the comprehensive overview that introduces all optical sensor types, explains what makes each one optical, and provides the framework for navigating the more detailed technology-specific, application-specific, and installation-specific articles in the cluster. It covers the seven key facts that define optical liquid level sensing, the five optical sensor types and the technology each one uses, the six applications where optical sensing delivers the most value, the four limitations and failure modes specific to optical sensing, the five critical specifications, and the five FAQs engineers and buyers ask most. It is the article that answers "what is an optical liquid level sensor and which one do I need."
Optical Liquid Level Sensors: Quick Answer
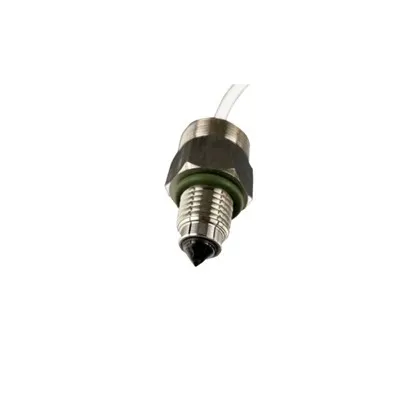
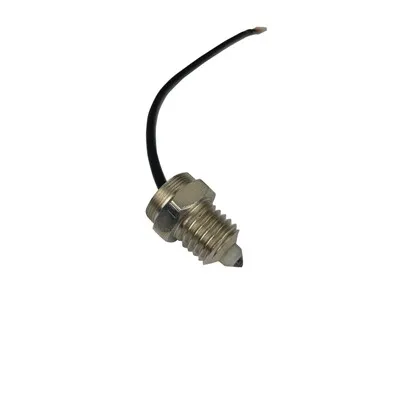
Optical liquid level sensors are liquid level sensors that use light - visible, infrared, or ultraviolet - to detect the presence of liquid or to measure the liquid level in a tank or vessel. "Optical" means the sensor's detection mechanism is based on the interaction between light and the liquid or the liquid-air interface: the sensor emits a beam of light, and the way the liquid or the liquid surface reflects, refracts, absorbs, or transmits that light is converted into a level signal. Optical sensors are distinct from mechanical sensors (float switches, vibrating forks), electrical sensors (conductive probes, capacitive sensors), ultrasonic sensors (which use sound rather than light), and pressure sensors (which use hydrostatic pressure). There are five main types of optical liquid level sensors: point-level switches using total-internal-reflection (TIR) in a prism tip, point-level switches using light refraction at a prism surface, continuous-level sensors using laser or LED triangulation, continuous-level sensors using fiber-optic distributed sensing, and continuous-level sensors using camera-based vision. Each type serves different measurement requirements: point switches detect a single high or low level (dry or wet); continuous sensors measure the level across the full tank height and output a 4–20 mA, HART, or digital signal proportional to the liquid height.
Seven Key Facts That Define Optical Liquid Level Sensing
What Makes a Sensor "Optical"
The seven key facts table (Featured Snippet):
| # | Fact | What it means | Why it matters |
|---|---|---|---|
| 1 | Optical sensors use light, not sound, electricity, or pressure | Light wavelength: 380–1,000 nm (visible + near-IR); sound frequency: 20 kHz–20 MHz | Light is unaffected by electrical interference, grounding issues, or pressure - optical sensors work where conductive or ultrasonic sensors fail |
| 2 | Optical sensors detect the liquid-air interface, not liquid conductivity | Detection is based on refractive index, reflection, or absorption - properties of light interacting with matter | Optical sensors detect non-conductive liquids (oils, solvents, fuels) that conductive sensors cannot detect |
| 3 | Optical point switches have no moving parts | The sensing element is a prism, a lens, a fiber, or a camera - no float, no vibrating fork, no mechanical contact | No moving parts means no mechanical wear, no pivot failure, and no product entrapment - ideal for sanitary and clean-in-place service |
| 4 | Optical sensors are inherently fast | LED response: microseconds; photodetector response: microseconds; total optical response: 1–10 ms | Fast enough for high-speed filling lines and rapid leak detection - faster than vibrating forks (50–500 ms) and floats (100–1,000 ms) |
| 5 | Optical sensors require a clean optical path | Prism surface, lens, or camera window must be free of contamination, biofilm, scale, or condensation | Dirty optics cause false readings - optical sensors require periodic inspection and cleaning in fouling environments |
| 6 | Optical sensors can be invasive or non-invasive | Invasive: prism inserted through tank wall; non-invasive: sensor mounted externally on transparent tank wall or sight glass | Non-invasive optical sensors eliminate tank penetration and maintain tank integrity - ideal for pharmaceutical and food applications |
| 7 | Optical continuous-level sensors use triangulation or TOF, not hydrostatic pressure | Level is calculated from the angle of reflected light (triangulation) or the time delay of a reflected light pulse (optical TOF) | Optical continuous sensors are unaffected by tank pressure, density changes, or vapor pressure - they measure the actual surface position |
Five Optical Sensor Types and the Technology Each One Uses
Point Switches and Continuous Sensors Across the Optical Spectrum
The five optical sensor types table (Featured Snippet):
| Sensor type | Measurement | Technology | Light source | Output | Best for |
|---|---|---|---|---|---|
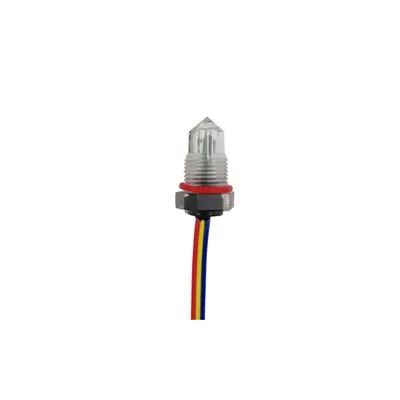
| TIR prism point switch | Point (dry/wet) | Total-internal-reflection disruption when prism is wet | Infrared LED (880–950 nm) | Relay, PNP/NPN, NAMUR | High/low alarms; leak detection; tank interior |
| Refraction point switch | Point (dry/wet) | Light refraction angle changes when liquid replaces air at prism tip | Visible red LED or infrared LED | Relay, PNP/NPN | Simple tanks; visual indicator variants; low-cost applications |
| Laser triangulation continuous sensor | Continuous (4–20 mA / digital) | Emits laser beam; detector measures angle of reflected beam; angle → level height | Visible red laser (630–680 nm) or infrared laser | 4–20 mA, HART, RS-485, Modbus | Precision continuous level; tanks with vapors and foam; non-contact measurement |
| Fiber-optic distributed sensor | Continuous (point array) | Multiple fiber-optic sensing points along a cable; each point is a TIR prism; all points connect to one controller | Infrared LED (shared light source) | Digital (multi-point addressable) | Multiple level points from one cable; large tanks; hazardous areas |
| Camera vision sensor | Continuous (visual) | CMOS/CCD camera captures images of liquid surface; image processing software calculates level | Ambient light or integrated LED backlight | Ethernet, RS-485, 4–20 mA (via gateway) | Complex tank geometries; interface detection; remote monitoring |
The five optical sensor types - TIR prism point switches, refraction point switches, laser triangulation continuous sensors, fiber-optic distributed sensors, and camera vision sensors - span the full range from simple dry/wet point detection to precision continuous level measurement with digital output, and each type uses a distinct optical mechanism to convert the light-liquid interaction into an electrical signal. TIR prism point switches (the most common optical level sensor type) use total-internal-reflection disruption: an infrared LED transmits light through the prism body to the prism tip; in air (dry), the light undergoes TIR and returns to the photodetector; in liquid (wet), the refractive index change at the prism-liquid interface disrupts TIR, less light returns, and the output switches. The prism material (borosilicate glass, n ≈ 1.47, or sapphire, n ≈ 1.77) determines the chemical compatibility and the TIR signal contrast. TIR switches are point-level only - they detect whether liquid is present at the prism tip position, not the level height. Refraction point switches use the change in the light refraction angle at the prism tip: the sensor emits a beam of light at a fixed angle; when the beam enters air, it refracts at a specific angle and misses the detector (dry, no signal); when liquid covers the prism tip, the refraction angle changes and the beam hits the detector (wet, signal). Refraction switches are simpler and lower-cost than TIR switches and are available with a built-in visual indicator (an LED that lights up when liquid is detected). Refraction switches are less sensitive than TIR switches and are more susceptible to false readings from prism contamination. Laser triangulation continuous sensors are the precision continuous-level option in the optical sensor family: the sensor emits a visible red laser beam (630–680 nm) at the liquid surface from a known angle; the detector inside the sensor measures the angle of the reflected beam; the angle is proportional to the distance from the sensor to the liquid surface, and the controller converts the angle into a level height using triangulation geometry. Laser triangulation sensors are non-contact and measure the actual liquid surface position continuously - they output a 4–20 mA analog signal, a HART digital signal, or a digital protocol (RS-485, Modbus) proportional to the level. The measurement accuracy is typically ±1–5 mm over a range of up to several meters. Laser triangulation is the preferred continuous optical method for tanks with significant vapor space, foam, turbulence, or condensing vapors - conditions where ultrasonic sensors (which use sound) struggle and where intrusive sensors (which contact the liquid) would be fouled. The key limitations are: the liquid surface must produce a diffuse reflection (mirror-like surfaces produce unreliable reflections); strong ambient light (direct sunlight, industrial lighting) can interfere with the detector; and the sensor must be mounted above the maximum liquid level with a clear line of sight to the surface. Fiber-optic distributed sensors use an array of optical sensing points along a single fiber-optic cable: each sensing point is a small TIR prism element; all points share a single infrared LED light source and a single photodetector controller; the controller measures the light returned from each point in sequence using time-domain reflectometry (a light pulse travels down the cable and the return time from each point is measured). Each point returns either full light (dry) or reduced light (wet), and the controller identifies which points are wet. The cable can have from 2 to 32 sensing points, providing multiple level detection points from a single cable installation. Fiber-optic distributed sensors are the optical solution for applications that require multiple level points (for example, detecting both a high-level alarm and a low-level alarm in a single tank from a single cable penetration) and for hazardous areas where electrical sensors are not permitted (fiber optics do not conduct electricity and are intrinsically safe). Camera vision sensors use a CMOS or CCD camera mounted above or inside the tank to capture images of the liquid surface. Image processing software analyzes the image to identify the liquid-air interface (using contrast, color, edge detection, or pattern recognition) and calculates the level height. Camera sensors provide the richest data output of any level sensor type: in addition to the level height, the camera sees foam depth, surface turbulence, interface position (in two-liquid tanks), wall fouling, and visual confirmation of the tank condition. Camera sensors are the preferred choice for complex tank geometries (horizontal tanks, spherical tanks, tanks with internal baffles) where non-contact continuous measurement is required, and for remote monitoring applications where visual confirmation of the level is required in addition to the level signal. The key limitations are: the camera window must be kept clean (oil vapor and product residue fog the window); the liquid surface must be visible (opaque products, dark oils, and tanks with significant vapor may be difficult for the camera to image); and the image processing software must be configured for the specific liquid, tank geometry, and lighting conditions.
Six Applications Where Optical Sensors Deliver the Most Value
Where the Light-Based Detection Advantage Is Decisive
The six applications table (Featured Snippet):
| Application | Optical sensor type | Key advantage over alternatives | Why light wins |
|---|---|---|---|
| Pharmaceutical tanks (WFI, bioreactors) | Reflective (non-invasive) or TIR prism; 3-A certified | No tank penetration; maintains sterility; CIP/SIP compatible | Fiber optics are the only intrinsically safe option; glass and sapphire prisms are chemically inert and produce no metallic contamination |
| High-purity water and chemical storage | TIR prism switch; laser triangulation for continuous | Detects non-conductive liquids; no electrodes to corrode; sapphire prism chemically inert | Conductive sensors cannot detect most chemical solvents; optical TIR detects any liquid with a different refractive index from air |
| Oil and fuel tanks | TIR prism switch (IP68); laser triangulation | Detects hydrocarbon liquids; explosion-proof housing available | Conductive sensors are completely blind to hydrocarbon fuels; optical TIR works in all fuel types |
| High-speed filling lines | TIR prism switch (1–10 ms response) | Fastest response of any point-level switch; no relay for sub-10 ms response | Vibrating forks (50–500 ms) and floats (100–1,000 ms) are too slow for high-speed filling |
| Multi-point large tank level | Fiber-optic distributed sensor | 2–32 points from one cable; single penetration; intrinsically safe | Running multiple individual switches requires multiple penetrations and complex wiring |
| Remote monitoring and IIoT integration | Camera vision sensor; laser triangulation with digital output | Visual confirmation + continuous signal + digital protocol integration | Camera provides the most complete tank status data for remote and automated monitoring systems |
Four Optical-Specific Limitations and Failure Modes
Why Optical Sensors Fail and How to Prevent It
The four optical limitations table (Featured Snippet):
| Limitation | Affected sensor types | Failure mode | Prevention |
|---|---|---|---|
| Prism or lens contamination (biofilm, scale, product residue) | TIR prism switches, refraction switches, camera vision | False wet reading when tank is dry - contamination mimics liquid at the optical surface | Specify sapphire prism for abrasive service; install in a protective shroud; schedule periodic prism cleaning; use CIP-compatible sensors in cleaning environments |
| Condensation or vapor on the sensing window | Reflective non-invasive switches, camera vision, laser triangulation | False wet reading (condensation disrupts light transmission); false dry reading (vapor changes refraction angle) | Ventilate the tank vapor space; use a purge or dry-air purge system on the sensor window; specify heated optics or anti-fog coating |
| Strong ambient light interference | Laser triangulation (direct sunlight), camera vision (glare) | Sensor sees ambient light instead of reflected signal - measurement error or false readings | Shield the sensor from direct sunlight; specify sensor with ambient light rejection algorithm; reposition the sensor to avoid direct glare from tank geometry |
| Opaque or dark liquids blocking light | Camera vision, laser triangulation (reflection-based) | Sensor cannot see the liquid surface - no measurement | Use TIR prism switches (detects via refractive index, not reflection); use ultrasonic or radar for opaque liquids; specify sensor with appropriate wavelength for the liquid color |
Five Critical Specifications for Optical Liquid Level Sensors
What to Look for on the Datasheet
The five critical specifications table (Featured Snippet):
| Specification | Typical range | Why it matters | How to verify |
|---|---|---|---|
| Measurement range | Point switches: N/A (fixed set point); continuous: 0.1–10 m (laser triangulation); 0.5–5 m (camera vision) | The sensor must cover the full tank height from the lowest to the highest expected level | Verify that the minimum and maximum range cover the tank dimensions and the minimum and maximum level positions |
| Accuracy | Point switches: ±1–5 mm (set point repeatability); continuous: ±1–10 mm (laser triangulation); ±2–20 mm (camera vision) | Accuracy determines whether the sensor meets the process control or alarm requirement | Specify accuracy at the operating temperature - accuracy degrades at temperature extremes |
| Light source wavelength | 630–680 nm (visible red laser); 850–950 nm (infrared LED for TIR); 400–700 nm (visible for camera backlight) | Wavelength determines penetration through vapor and color sensitivity for camera sensors | Specify infrared (near-IR) for vapor environments (infrared penetrates water vapor better than visible light); specify visible for camera sensors to match human-visible contrast |
| Operating temperature range | –40°C to +80°C (standard); –40°C to +120°C (extended); up to +200°C (with extension neck) | The sensor must survive the maximum temperature - including SIP, CIP, and summer high-temperature conditions | Verify at the maximum operating temperature, not the design temperature; derate at elevated temperature if required |
| Hazardous area certification | Non-hazardous; ATEX/IECEx; FM; CSA; Intrinsically Safe (Ex ia); Non-incendive (Ex nA) | Electrical sensors (laser, camera) may not be permitted in hazardous areas without certification; fiber-optic sensors are inherently safe | Specify ATEX/IECEx certified sensor for gas and vapor hazardous areas (Zone 0, 1, 2); fiber-optic distributed sensors are inherently safe and require no hazardous-area certification for the sensing element |
Five FAQs
Q1: What is the difference between an optical liquid level sensor and an ultrasonic level sensor?
The fundamental difference is the physical phenomenon the sensor uses to detect the liquid surface: an optical sensor uses light (electromagnetic waves with wavelengths of 380–1,000 nm), and an ultrasonic sensor uses sound (mechanical pressure waves with frequencies of 20 kHz–20 MHz). This difference drives every practical consequence. Light travels at approximately 3×10⁸ m/s and is unaffected by electrical noise, grounding, or electromagnetic interference. Sound travels at approximately 343 m/s in air at 20°C and is affected by temperature, vapor composition, wind, and acoustic noise. Optical sensors measure the position of the liquid surface using reflection or refraction; ultrasonic sensors measure the position using the time-of-flight of a sound pulse (time = 2×distance/speed of sound). Ultrasonic sensors are slower (response time 100 ms–2 s vs 1–10 ms for optical), are affected by temperature changes (the speed of sound changes by approximately 0.6 m/s per °C, which requires temperature compensation), and struggle with foam and condensing vapors (which scatter and absorb sound). Optical sensors are faster, more precise, and unaffected by temperature, but they require a clean optical path (prism contamination blocks light) and are limited to line-of-sight installations (the light beam must reach the liquid surface). The practical rule: use ultrasonic for simple open-tank continuous level measurement where the liquid surface is calm and the vapor space is clean; use optical for precision measurement, fast response, non-conductive liquids, or environments where sound-based measurement is unreliable.
Q2: Can optical liquid level sensors be used in hazardous areas?
Yes - but the certification requirements differ by sensor type and the hazardous area classification. TIR prism point switches with relay outputs are available with ATEX/IECEx explosion-proof certification (Ex d - flameproof enclosure) or intrinsically safe certification (Ex ia - suitable for Zone 0). The explosion-proof relay output version uses a flameproof enclosure that contains any ignition source inside the housing; the intrinsically safe version limits the electrical energy to a level below the ignition energy of the flammable atmosphere. Fiber-optic distributed sensors are the preferred optical solution for hazardous areas: fiber optics do not conduct electricity, so the sensing element (the fiber-optic cable with TIR prism sensing points) is inherently safe and requires no hazardous-area certification. Only the controller at the non-hazardous end of the fiber requires certification. Laser triangulation continuous sensors and camera vision sensors are electrical sensors and require ATEX/IECEx certification for hazardous area installation. The laser in a triangulation sensor is typically Class 2 (<1 mW) or Class 3R (<5 mW) and may not be permitted in Zone 0 or Zone 1 areas without additional protective measures. Camera vision sensors in hazardous areas require explosion-proof housings and may have limited operating temperature ranges due to the heat generated by the camera electronics. For Zone 0 (continuous hazardous atmosphere) applications, fiber-optic distributed sensors or intrinsically safe TIR prism switches are the recommended optical solutions.
Q3: How do optical liquid level sensors perform in steam-filled tanks?
Optical liquid level sensors in steam-filled tanks face two primary challenges: condensation on the optical surface and temperature limits. Condensation on the prism surface or camera window acts as a liquid layer and disrupts the optical signal - condensation on a TIR prism causes the same refractive index change as liquid contact, producing a false wet reading. Condensation on a camera window fogs the image and prevents the software from identifying the liquid surface. The mitigation is a dry-air purge system: a small quantity of instrument air is piped to the sensor and flows past the prism or window, preventing condensation. The purge air flow rate is typically 1–5 L/min and requires a clean, dry instrument air supply. Temperature limits are the second challenge: most optical switches are rated to 80°C–120°C, but steam-filled tanks at atmospheric pressure reach 100°C and pressurized steam reaches 121°C–134°C (SIP conditions). Extended temperature-rated sensors (rated to 150°C–200°C with a stainless steel extension neck that distances the electronics from the steam zone) are available for SIP applications. Sapphire prisms are preferred over glass prisms in steam service because sapphire is harder, more thermally stable, and less susceptible to thermal shock cracking.
Q4: What is the typical lifespan of an optical liquid level sensor?
The expected lifespan of an optical liquid level sensor depends on the sensor type and the operating environment. TIR prism point switches have the longest expected lifespan of any level switch technology because they have no moving parts and no consumable elements: the LED, photodetector, and signal processing electronics are solid-state components with a typical operating life of 50,000–100,000 hours (approximately 6–11 years at continuous operation). The prism and housing are the components most subject to wear - prism contamination (biofilm, scale, product residue) is the primary cause of optical switch failure, not electronic aging. Scheduled cleaning and periodic functional testing extend the sensor life indefinitely. Laser triangulation sensors have a typical lifespan of 5–10 years for the laser diode (the laser output degrades by approximately 1–2% per year, and the sensor accuracy specification must be maintained above the minimum acceptable level). Camera vision sensors have a typical lifespan of 3–7 years for the camera module, with the LED backlight (for backlit configurations) being the most common component to fail before the camera itself. Fiber-optic distributed sensors have the longest lifespan because the fiber cable and the prism sensing elements are passive optical components with no electronics at the sensing point: the fiber cable is rated for 20–30 years in most industrial environments, and the only lifespan-limited component is the controller light source and detector (typically 5–10 years).
Q5: How do I choose between a point-level optical switch and a continuous optical level sensor?
The point vs continuous optical comparison table (Featured Snippet):
| Criterion | Point-level optical switch | Continuous optical level sensor |
|---|---|---|
| Measurement type | Binary: dry (below set point) or wet (above set point) | Continuous: level height across the full tank range |
| Number of level points | One set point per switch; multiple switches required for multiple points | One sensor measures the full range continuously |
| Output signal | Relay contact (dry/wet) or discrete transistor signal | 4–20 mA, HART, RS-485, Modbus, Ethernet |
| Cost | Lower cost per point | Higher initial cost, but one sensor replaces multiple switches |
| Wiring complexity | One cable per switch | One cable per sensor |
| Best for | High-level alarm, low-level (dry-run) alarm, overfill protection, leak detection | Inventory management, process control, filling control, batch monitoring |
| Set point adjustment | Fixed (fixed-tip) or field-adjustable (adjustable-tip) | Software-configurable or mechanically adjustable sensor height |
Choose a point-level optical switch when the application requires only one or two discrete detection points (high alarm, low alarm), when the alarm response is a binary action (stop the pump, trigger an alarm), when the budget is limited, and when the detection point is fixed and known at the design stage. Choose a continuous optical level sensor when the application requires the actual level height at all times (for inventory, process control, or filling optimization), when the level must be monitored and recorded continuously, when the system requires a proportional control signal (4–20 mA proportional to level), or when the level height must be visible on a display or SCADA system. A typical process tank uses both: a continuous optical level sensor for continuous monitoring and inventory, and one or two point-level optical switches for high-level overfill protection and low-level dry-run protection (the point switches serve as the redundant safety system required by most regulatory standards).
The Bottom Line
Optical liquid level sensors are sensors that use light - not sound, electricity, or pressure - to detect or measure liquid level, and the choice between the five optical sensor types (TIR prism switch, refraction switch, laser triangulation, fiber-optic distributed, and camera vision) is driven by whether the application requires point-level detection or continuous measurement, how many detection points are needed, whether the environment is hazardous, and what the output signal must be. TIR prism point switches are the workhorse of the optical sensor family: fast (1–10 ms), reliable, no moving parts, and compatible with both conductive and non-conductive liquids. Laser triangulation continuous sensors are the precision option: ±1–5 mm accuracy, non-contact, and continuous 4–20 mA or digital output. Fiber-optic distributed sensors are the solution for multi-point level monitoring and hazardous areas: 2–32 sensing points from one cable, with inherently safe fiber optics throughout. Camera vision sensors are the most information-rich option: continuous level plus visual confirmation of foam, surface turbulence, and tank condition. The five critical specifications - measurement range, accuracy, light source wavelength, operating temperature, and hazardous area certification - are the parameters to verify on every datasheet. The four optical-specific failure modes - prism contamination, condensation, ambient light interference, and opaque liquids - require specific mitigation strategies and must be considered during sensor selection and installation. The one-sentence rule: optical liquid level sensors are the right choice for fast, precise, non-contact, non-conductive-liquid level detection - but the sensor type must match the measurement requirement (point vs continuous), the output must match the control system (relay vs 4–20 mA vs digital), and the optical path must be protected from contamination, condensation, and opaque liquids.
Last updated: August 2026
Disclaimer: This article is a general educational overview of optical liquid level sensors and their technologies. Specifications, measurement ranges, accuracy values, and application guidelines are general engineering reference data and do not apply to every specific product or installation. Sensor selection, installation, wiring, and maintenance must be performed by qualified engineering and maintenance personnel in accordance with the specific sensor manufacturer's datasheet and installation instructions and the applicable industry standards. Hazardous-area certification requirements must be verified against the specific flammable substance, temperature class, and zone classification for the installation. Chemical compatibility of wetted materials must be verified against the Safety Data Sheet (SDS) for the specific liquid, concentration, and operating temperature. This article does not constitute engineering design, regulatory compliance, or safety certification advice.